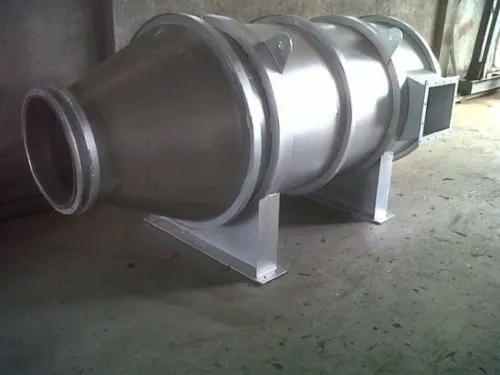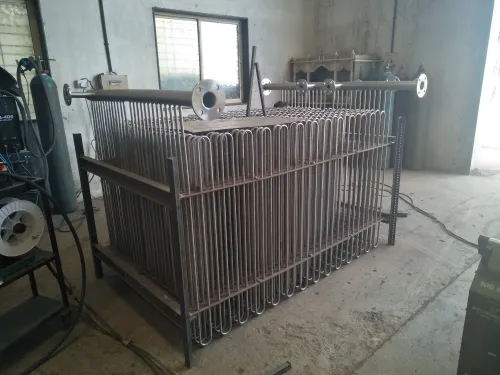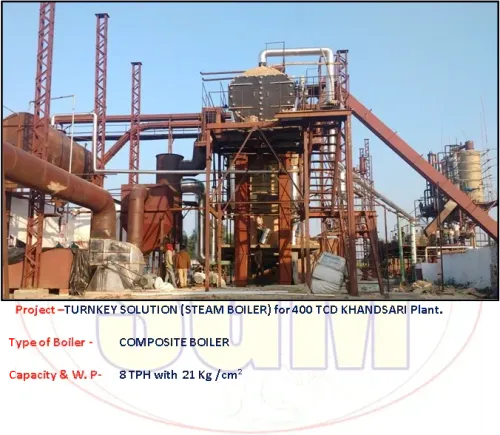
A boiler air preheater can recover heat from flue gas, but its value depends on operating hours, fuel cost, moisture in bagasse, fan capacity and the temperature you can safely deliver to the furnace. You will be able to estimate recoverable heat, test payback, compare designs and identify the scope details behind an air pre heater cost for jaggery plant in Pune.
Key takeaways
- Use an air preheater when seasonal fuel savings can repay its installed cost.
- Size heat duty from flue-gas flow, temperatures, combustion air and furnace limits.
- Choose a compact recuperative exchanger for many small or seasonal jaggery plants.
- Compare quotations using heat recovery, pressure drop, materials, controls and commissioning scope.
When does a boiler air preheater make sense in a jaggery plant?
Install a boiler air preheater only when the jaggery season provides stable operating hours, worthwhile fuel value and enough recoverable flue-gas heat to repay the equipment. Boiler flue gas passes through one side of the exchanger and heats combustion air on the other side before that air reaches the furnace or burner.
Base the decision on measured plant conditions:
- Fuel consumption per hour and jaggery-season operating hours
- Current flue-gas temperature and measured flue-gas flow
- Combustion-air flow and desired air temperature
- Usable recovered duty after pressure-drop and fouling allowances
- FD and ID fan flow, static-pressure margin, motor loading and dirty-condition performance
A rated boiler capacity is not enough. Wet bagasse consumes heat evaporating moisture; changes in particle size, ash content or feeding rate alter combustion and flue-gas temperature. A heat balance based only on the nameplate rating can promise recovery the furnace cannot deliver.
Air preheater for jaggery plant and economizer recover heat in different places:
| Option | Heat goes to | Compare using |
|---|---|---|
| Boiler air preheater | Combustion air | Same stack temperature and fan-power assumptions |
| Economizer | Boiler feedwater | Same stack temperature and fan-power assumptions |
Choose the option with higher usable duty and stronger seasonal payback, not the higher catalogue efficiency. If the boiler cycles frequently, runs at low load or burns nearly free bagasse, the added exchanger, ducting and fan power may not justify installation.
How do you size the heat duty without overheating the furnace?
Size the duty from measured operating data, not boiler nameplate capacity. Use Q = combustion-air mass flow × air specific heat × air-temperature increase, with air mass flow and temperatures recorded at representative low, normal and high loads. This gives a usable heat-duty range for an air preheater for jaggery plant applications.
1. Measure combustion-air flow, inlet temperature and desired outlet temperature at each load. Convert the result to kW using air specific heat, then select a controlled outlet-temperature range rather than the highest temperature the exchanger can produce.
2. Test sugarcane bagasse, wood, coal, husk and mixed agro-waste for moisture, ash and fuel variability. Wet fuel reduces useful heat; ash loading and particulate carryover foul heat-transfer surfaces, restrict passages and increase pressure drop.
3. Protect grates, burners, refractory, ducts, seals and feeding equipment with a bypass or tempering damper. Install an outlet thermocouple, high-temperature interlock and cold-start protection so the preheater cannot send hot air to an unheated furnace or empty feed system.
4. Keep the flue-gas outlet above the effective water and contaminant condensation limit established from fuel analysis and actual gas composition, including cold start and low-load operation. Excessive cooling creates sticky deposits, plugging and corrosion.
5. Check FD and ID fan capacity under dirty conditions before approval. Preheating air does not guarantee particulate compliance; poor combustion, unburned bagasse, ash carryover or inadequate dust collection can still breach emission limits.
Which air-preheater arrangement suits a small or seasonal Pune plant?
A gas-to-air tubular recuperative unit usually suits a small or seasonal Pune jaggery plant better than a rotary regenerative heater. Separate gas and air passages keep the design simple, with fewer moving parts, no rotor seals and less leakage risk during shutdowns and intermittent operation.
| Option | Heat-transfer arrangement | Best fit |
|---|---|---|
| Tubular recuperative | Fixed tubes keep flue gas and combustion air separate | Small plants, seasonal duty and easier cleaning |
| Rotary regenerative | A moving matrix carries heat between gas and air streams | High gas flow, long operating hours and substantial recovered duty |
Bagasse ash and alkali deposits can block heat-transfer surfaces and increase pressure drop. Specify access doors, removable tube bundles or elements, soot-blowing or mechanical cleaning, low-point drains and a defined cleaning schedule based on operating experience.
Check both exchanger-side fans before approving the design:
- Confirm flue-gas and combustion-air flow at minimum, normal and maximum load.
- Verify static-pressure margin with clean and dirty pressure drops.
- Check motor loading after installation, not only from nameplate ratings.
- Test dirty-condition performance so draft and furnace air remain stable.
A rotary unit earns consideration when high gas flow and long operating hours produce enough recovered duty to fund rotor, seal and drive maintenance. Do not judge an industrial air pre heater price from exchanger surface area alone; cleaning access, fan changes and downtime can dominate the lifecycle cost.
How do you calculate payback instead of assuming efficiency savings?
Payback is the value of fuel or production gained during the jaggery season, minus every cost created by the preheater. Use this calculation: (fuel saved per hour × operating hours × usable value of displaced fuel) − extra FD and ID fan electricity − maintenance − cleaning labour − production losses during downtime.
Divide the installed cost by the resulting seasonal or annual benefit.
Value bagasse honestly. If it is an internal, nearly free fuel, a catalogue efficiency percentage has little financial meaning; count avoided purchased fuel, reduced auxiliary fuel, additional jaggery production or more stable combustion instead. Include the exchanger, ducts, dampers, insulation, supports, controls, fan modifications, installation, commissioning time and taxes.
A quotation for air pre heater cost for jaggery plant in pune is incomplete without these items.
Check the calculation against operating reality:
- Use low-load, normal-load and full-load fuel rates, not boiler nameplate capacity.
- Deduct downtime during installation and commissioning, plus cleaning labour caused by expected bagasse-ash fouling.
- Recalculate with wet bagasse, fewer jaggery-season hours, higher pressure drop and lower recovered duty.
- Add electricity for fans operating under dirty conditions, where draft or combustion-air flow falls.
- Test frequent cycling and batch operation separately; heat recovered during short runs may never repay startup losses.
The project is difficult to justify when fuel is nearly free, the boiler runs intermittently, or existing FD and ID fans have little spare capacity. These checks produce a defensible air pre heater cost for jaggery plant in pune rather than a percentage-based assumption.
How should you compare Pune supplier quotations?
Do not compare quotations by exchanger area or efficiency percentage. Ask every air pre heater supplier in Pune to price the same measured operating case and document:
- Guaranteed heat-recovery duty, flue-gas flow and temperature, combustion-air flow and outlet temperature at minimum and maximum load, clean and dirty pressure drops, leakage assumptions, fouling allowance, materials, corrosion protection and performance-test conditions.
- Inspection access, cleaning method, fan power impact and the required FD and ID fan margin. A quotation without dirty-condition data cannot show whether the plant will retain furnace draft after ash builds up.
| Scope | Included work | Cost consequence |
|---|---|---|
| Equipment only | Exchanger, casing, basic instruments and factory testing | Excludes site integration and many installation costs |
| Complete package | Exchanger, ducts, FD or ID fan changes, bypass and isolation dampers, insulation, supports, access platforms, thermocouples, control panel, fire and combustible-dust safeguards, erection and commissioning | Add taxes and production downtime separately |
Request a written NFPA 652 combustible-dust hazard review covering spark or flame carryover, dust accumulation, temperature monitoring, shutdown logic and isolation. Assess whether NFPA 85 applies to the combustion-system scope. Record who supplies each safeguard.
There is no defensible single industrial air pre heater price or air pre heater cost for jaggery plant in Pune without these boundaries. SGM Tech can be considered when you need a Pune-based integrator to coordinate the exchanger, ducting, controls, installation and commissioning; select on documented guarantees and lifecycle cost.
Related products
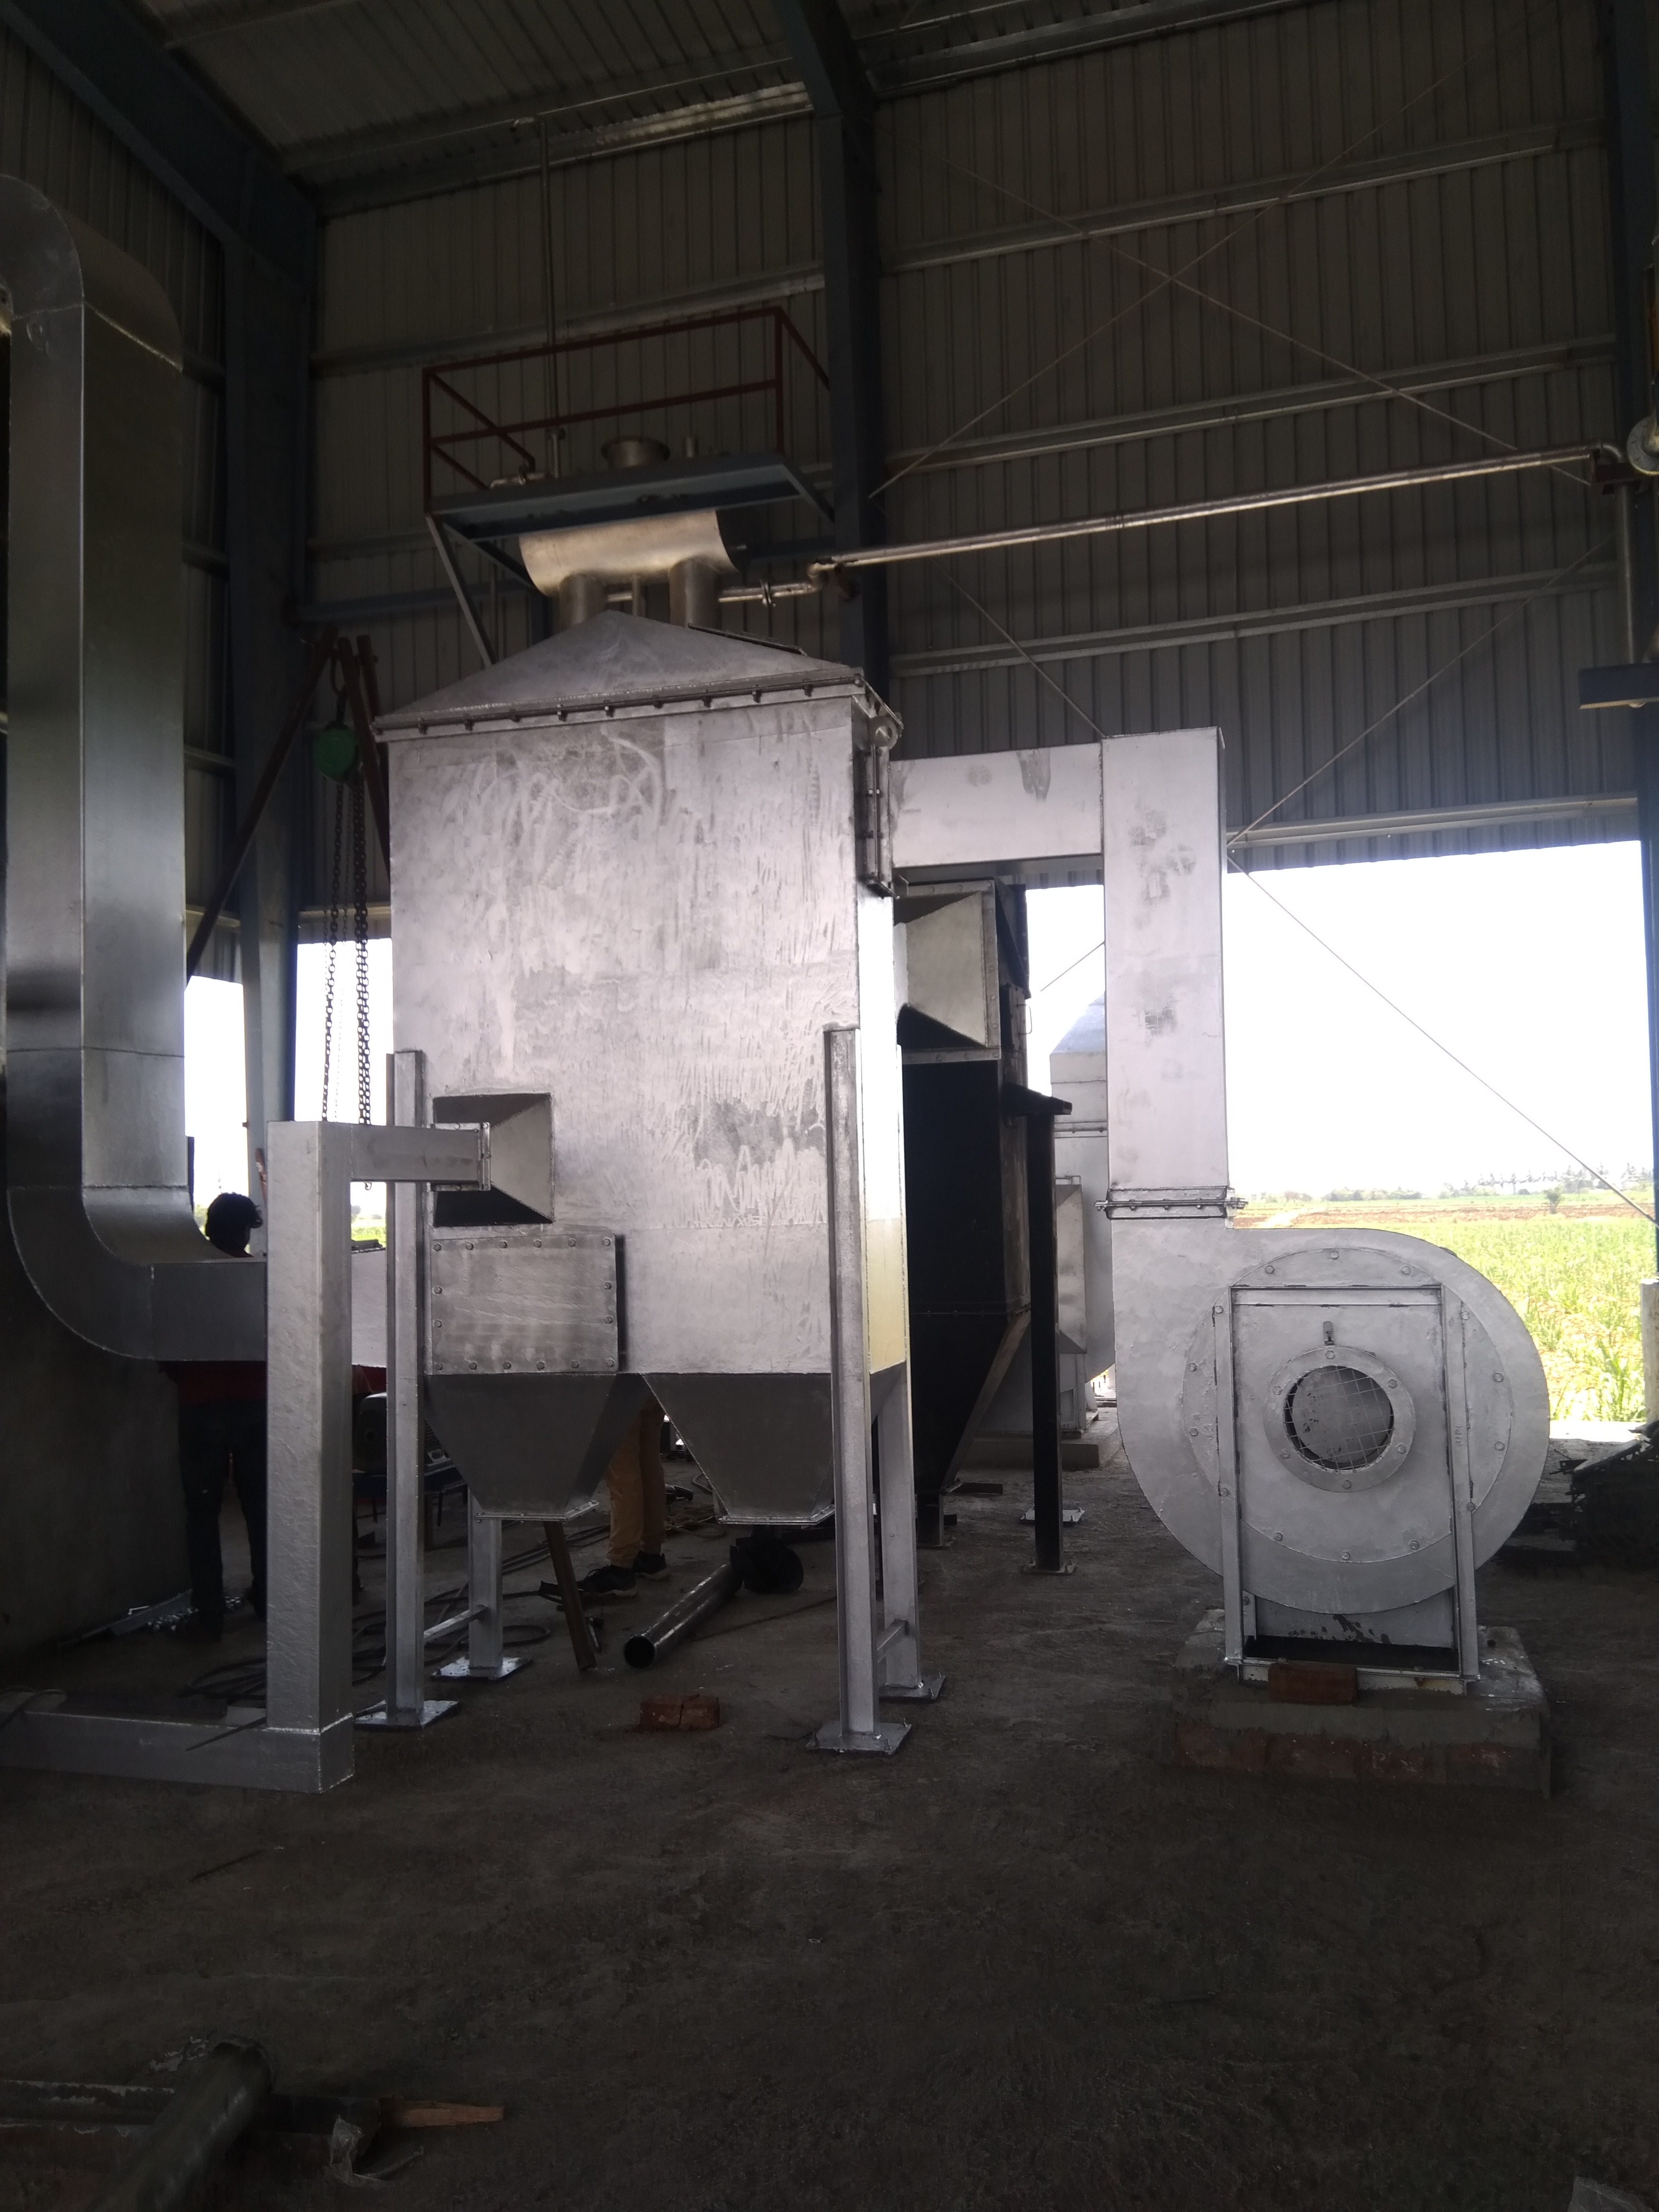 | AIR PRE HEATER An AIR PRE-HEATER (APH) is any device designed to heat air before another process (for example, combustion in a boiler) with the primary objective of... View product → |
 | JAGGERY MANUFACTURERS IN PUNE JAGGERY is a product derived from sugarcane juice by removing water content from it. View product → |
Frequently asked questions
When does a boiler air preheater make sense in a jaggery plant?
It makes sense when the plant has stable seasonal operating hours, valuable fuel savings and enough flue-gas heat after boiler operation and draft requirements.
How do you size an air preheater without overheating the furnace?
Calculate heat duty from flue-gas and combustion-air flow, inlet temperatures, target outlet temperature, allowable pressure drop and the furnace’s maximum air-temperature limit.
Which air-preheater arrangement suits a small or seasonal Pune plant?
A compact recuperative air preheater with separated flue-gas and air passages suits many small plants because it has no rotating seals and is easier to isolate during shutdowns.
How do you calculate air-preheater payback?
Convert recovered heat into fuel saved per operating hour, multiply by verified seasonal hours and fuel cost, then compare annual savings with equipment, installation, maintenance and downtime costs.
How should you compare Pune air-preheater supplier quotations?
Compare quoted heat duty, gas and air temperatures, pressure drop, materials, soot-cleaning access, bypass arrangements, instruments, warranty, installation scope and commissioning tests.
Related products
 | HOT AIR A HOT AIR GENERATOR is a type of heater in which heat is generated by burning fuel and is transferred to the air at ambient temperature which is then... View product → |
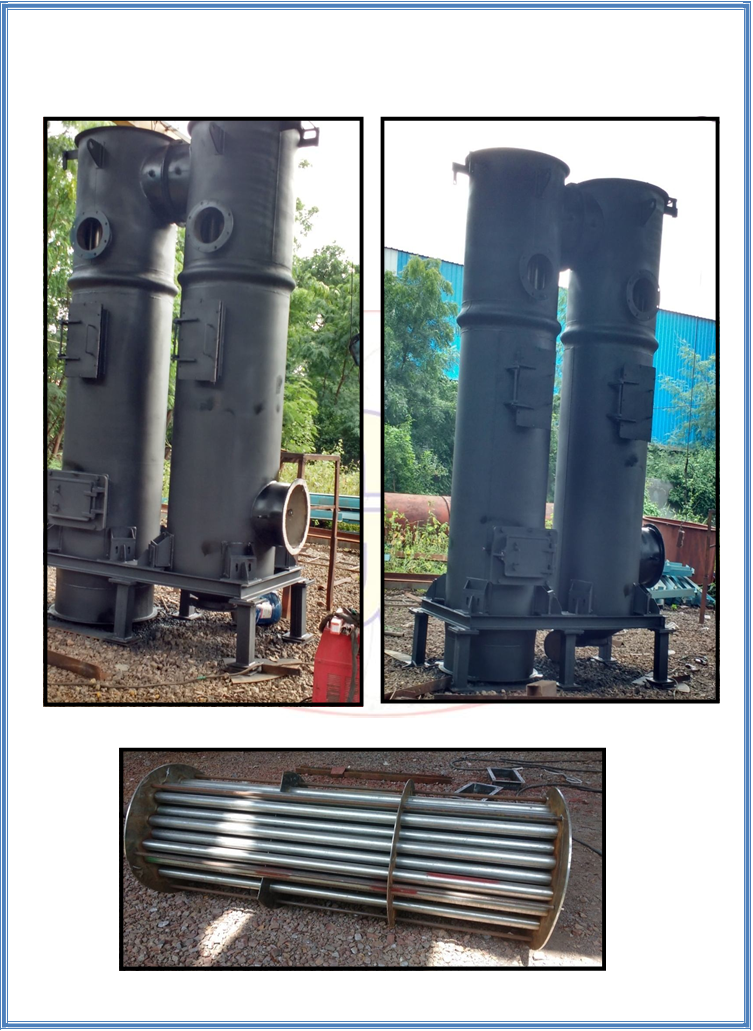 | WASTE HEAT RECOVERY A RECUPERATOR is a special purpose counter-flow energy recovery AIR HEAT EXCHANGER positioned within the supply and exhaust air streams of an air... View product → |
 | SUPER HEATER A SUPER HEATER is a device used to convert saturated steam or wet steam into super-heated steam or dry steam. View product → |
 | THERMAL OIL HEATER A THERMIC FLUID HEATER is an industrial heating equipment, used where only heat transfers are desired instead of pressure. View product → |